Skip to content
R.K./Engg.

Sheet 02 — Projects

Five
programmes.

Each one a family of parts we run in volume for automotive customers. Real parts, photographed on our own benches.
Precision bushes & sleeves
01

RK-01

Precision bushes & sleeves

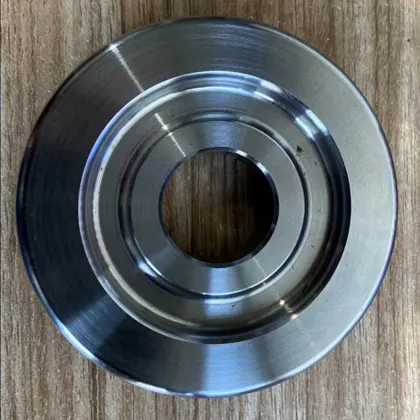
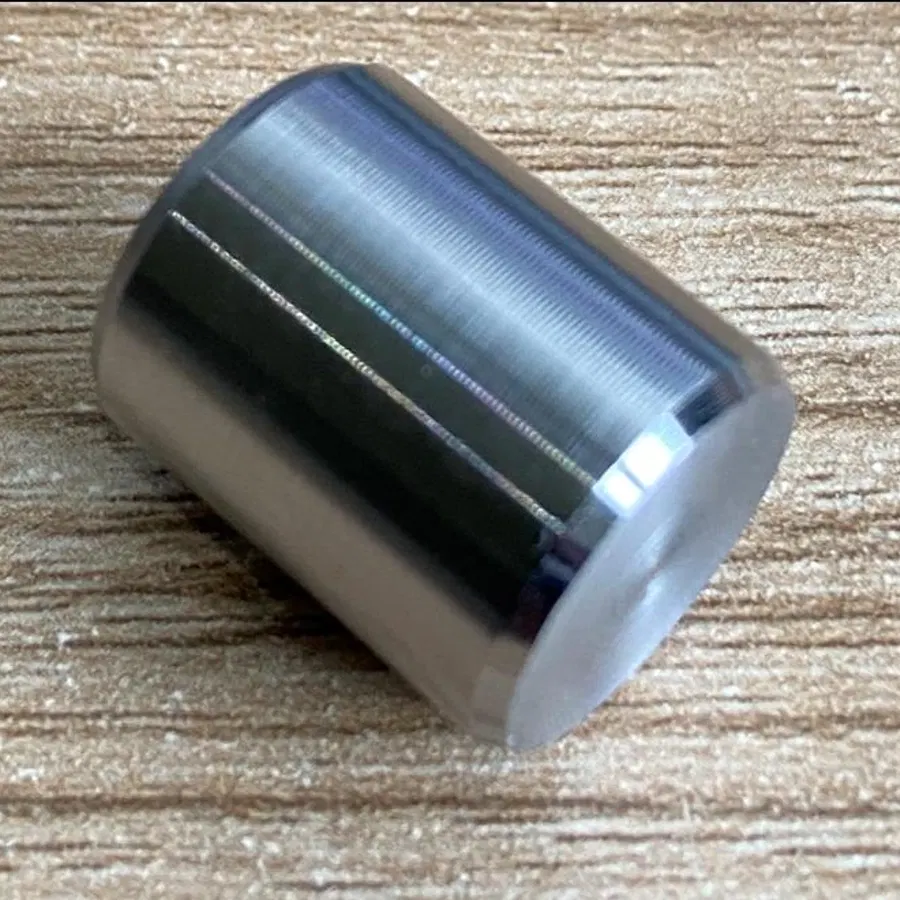
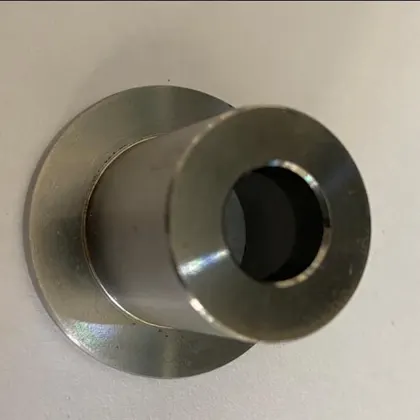
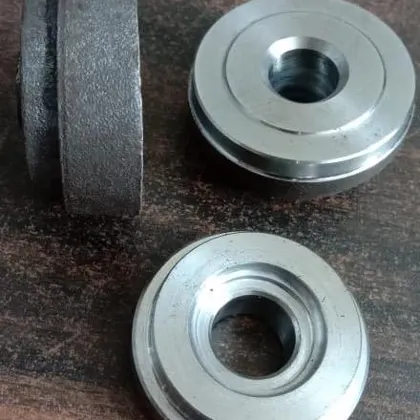
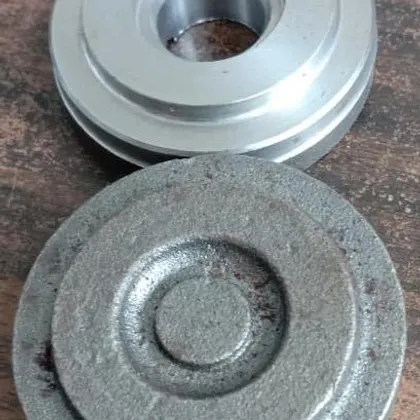
Our signature part. Forged blanks turned, bored and faced on CNC, with the bore held to a 13 micron tolerance band.

Bushes are where a machine shop shows its hand. The bore has to sit dead concentric to the outside diameter, the faces have to be square, and the tolerance leaves no room for a tired tool. Every bush programme at R.K. runs on CNC with a dedicated gauge for each operation — including the small ones — so a drift is caught at the machine, not at the customer's goods-inward.

ID tolerance
13 µm
Start stock
Forged blank
Check
Air gauge, 100%

Route

  1. CNC turning
  2. Boring
  3. Facing
  4. Air-gauge inspection

Supplied to

Tightwell Group · JCBL / MSL · Deepak Fasteners (Unbrako) · Allena Auto · Shree Patel Industries
Hardened components
02

RK-02

Hardened components

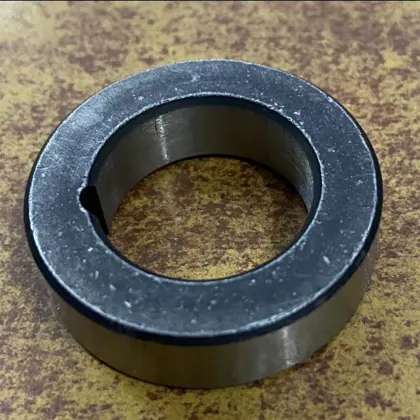
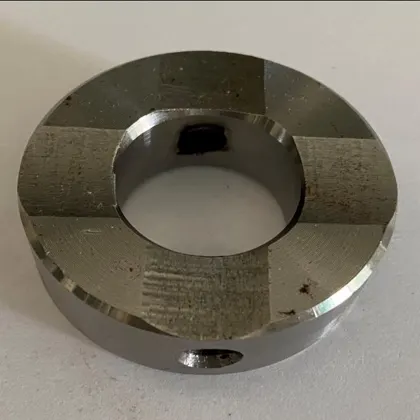
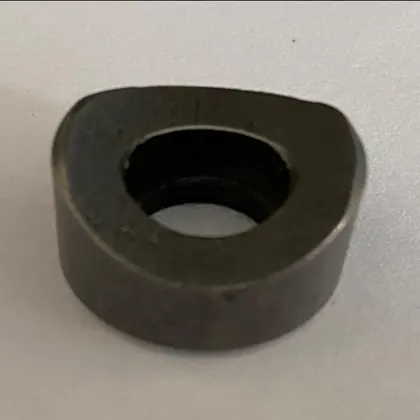
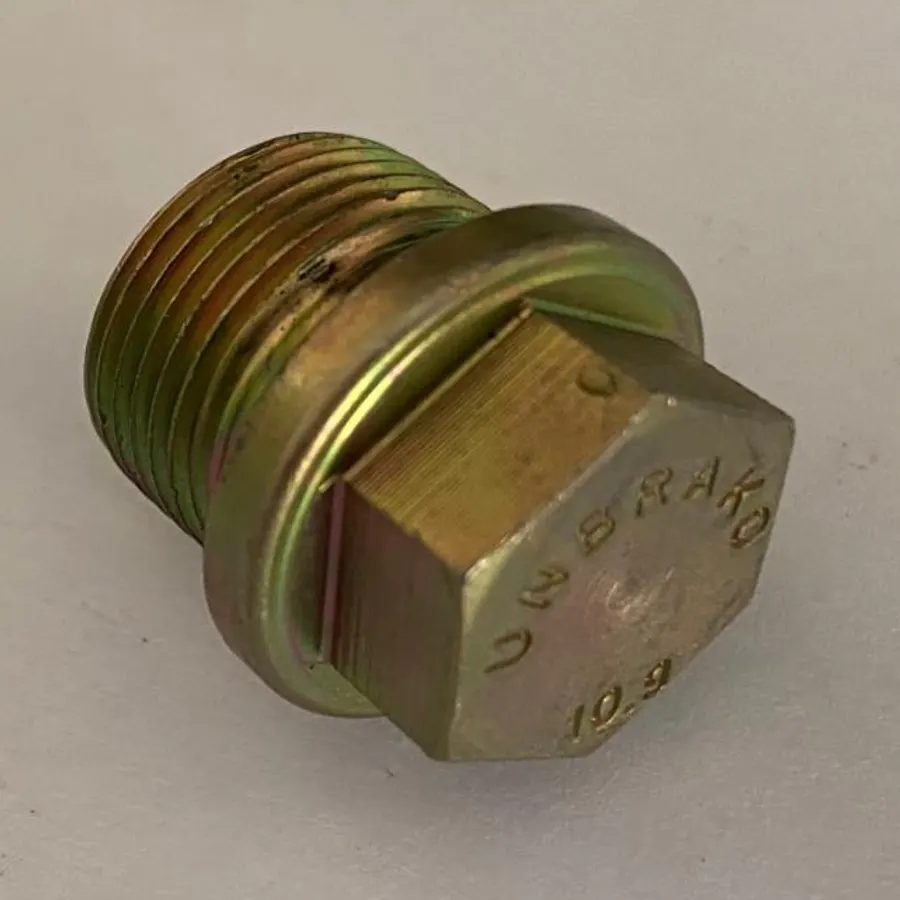
Parts hardened before machining — plug screws, stepped washers and rings that must hold their geometry through heat treatment and after it.

Machining after hardening is slower and less forgiving: tool wear climbs, heat builds, and any chatter shows on the surface. It's also the only way to guarantee the final dimension is the one that ships. The Unbrako 10.9 plug screw in this programme is the proof — thread form, hex and seat all checked on the profile projector before a lot is released.

Condition
Hardened pre-machining
Grade shown
10.9 plug screw
Check
Profile projector

Route

  1. Hardening
  2. Hard turning
  3. Grinding
  4. Profile projection

Supplied to

Deepak Fasteners (Unbrako) · Dynamic Transmission Group

Plated components
03

RK-03

Plated components

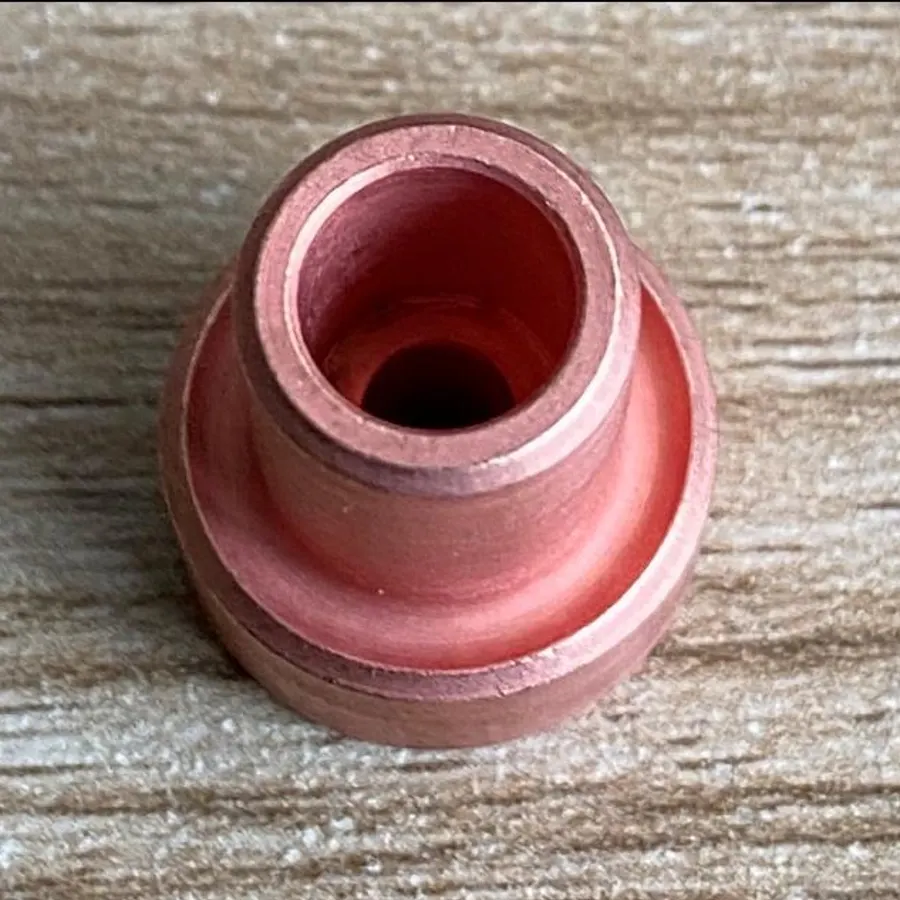
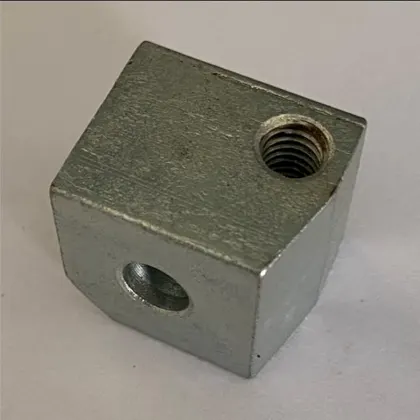
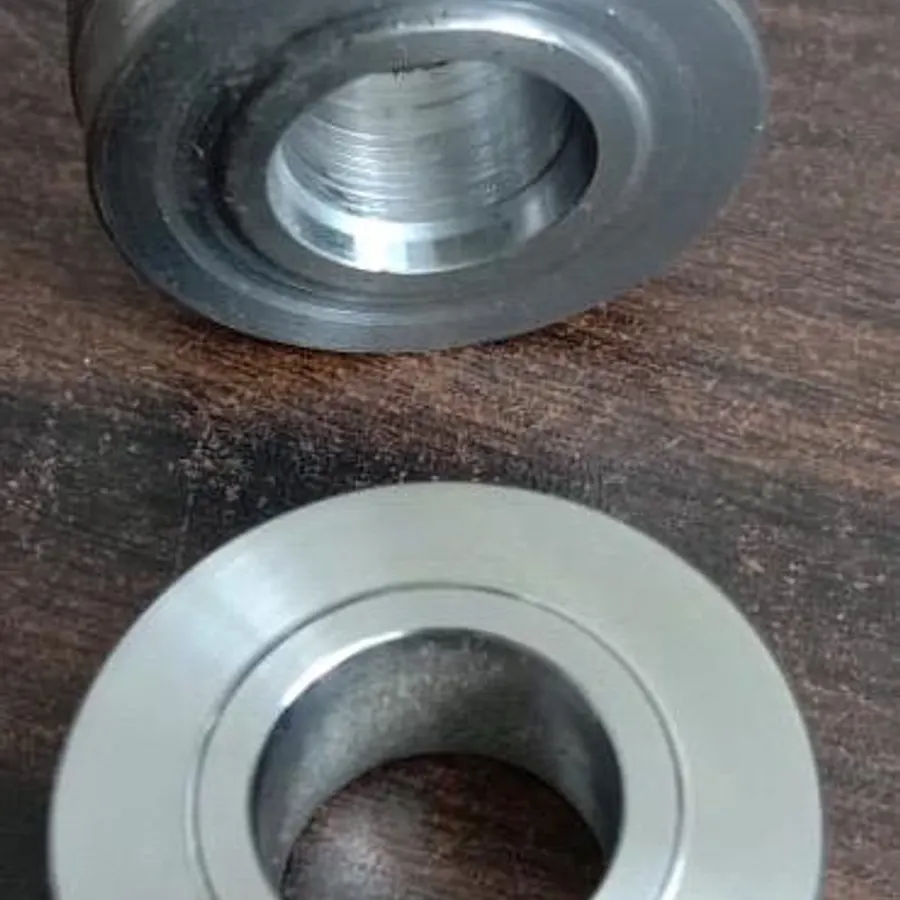
Threaded adaptors, sleeves and brackets finished in zinc-yellow, clear zinc and copper, with plating allowance machined in from the start.

A thread that gauges perfectly in the white can refuse a nut once it comes back from the plater. Our plated programmes are machined with the coating thickness already accounted for, and threads are gauged twice — before the parts leave for plating and again when they return.

Finishes
Zinc-yellow · Zinc · Copper
Features
Internal & external threads
Check
Thread gauges pre & post plating

Route

  1. Turning
  2. Threading
  3. Drilling & tapping
  4. Plating

Supplied to

Tightwell Group · Shree Patel Industries

Turned & ground parts
04

RK-04

Turned & ground parts

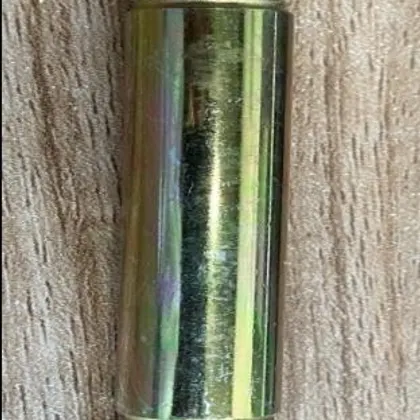
Dowels, pins, shafts and adjusters — turned on single-spindle Traubs and CNC, then finished on centreless grinders for a true round.

Fourteen single-spindle Traub machines keep the high-volume pins and dowels moving, while the centreless grinders take them the last few microns to size. It's an old-school pairing that still beats almost anything on cost-per-part for simple cylindrical work.

Bar capacity
Ø25 & Ø32 Traub
Finish
Centreless ground
Check
0–25 & 25–50 mm micrometers

Route

  1. Single-spindle turning
  2. Centreless grinding
  3. Milling
  4. Micrometer check

Supplied to

Dynamic Transmission Group · Sebrose Auto Pvt. Ltd. · JCBL / MSL · Allena Auto

Sleeves, nuts & keys
05

RK-05

Sleeves, nuts & keys

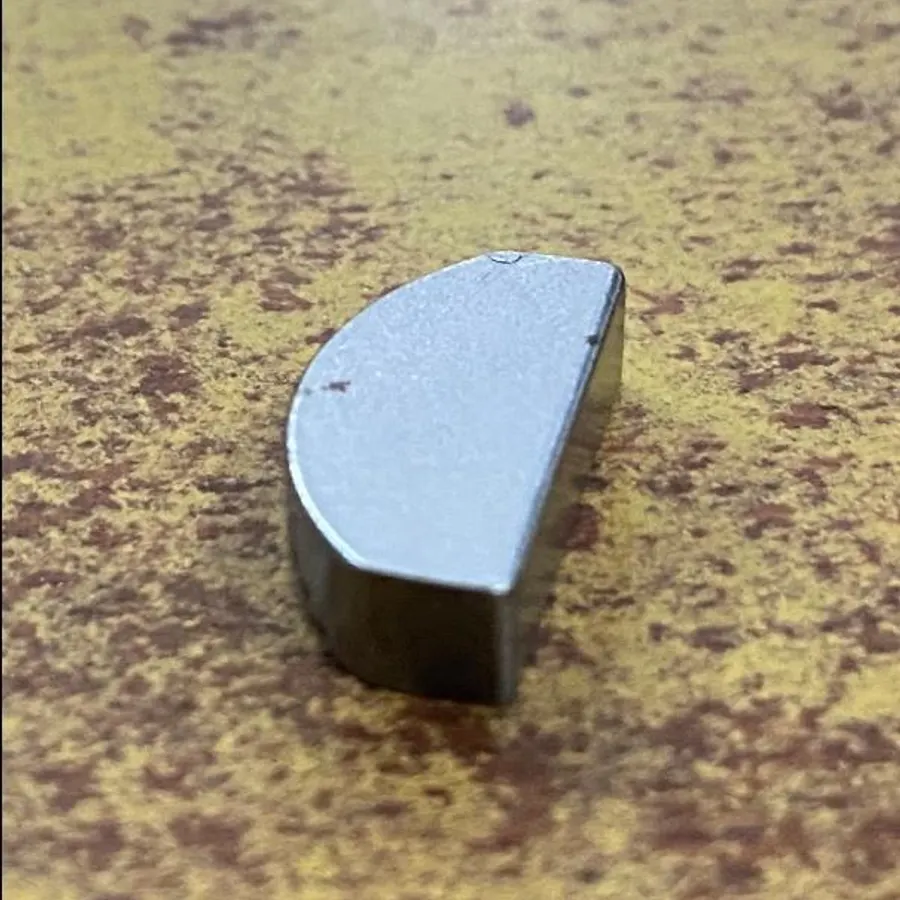
The small parts that stop a gearbox from coming apart: woodruff keys, lock nuts, taper sleeves and head top nuts.

Nobody notices a woodruff key until one shears. These programmes are low on glamour and high on consequence, so every bin carries a material identification tag with customer, part number, operation performed, next operation, quantity, lot number and a supervisor's signature.

Range
Keys · Lock nuts · Taper sleeves
Finish
Surface ground where specified
Traceability
Lot-tagged per bin

Route

  1. Turning
  2. Milling
  3. Surface grinding
  4. Visual & gauge inspection

Supplied to

Tightwell Group · Dynamic Transmission Group · Aurangabad Auto Engg. P. Ltd.

Got a part that’s giving your current vendor trouble?

Send the drawing